Paragweld - Welding Machine Manufacturer in India

Parag Traders was established in GIDC, Vatva, Ahmedabad in 1980 by Mr.Parag Mashruwala to cater to the requirement of welding electrodes, equipments™ and accessories.

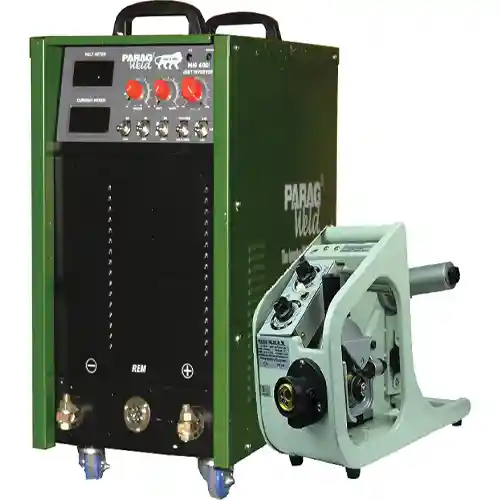
Paragweld MIG Series

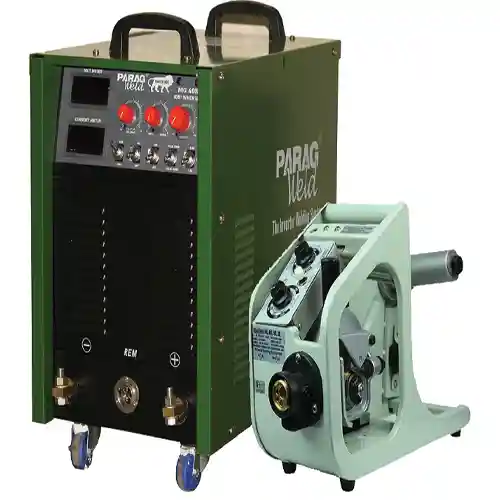
Paragweld MIG Series

Industrial MIG/MAG welding (GMAW) feeds a continuous wire through the torch while a shielding gas, usually CO2 or an argon mix, protects the weld pool. The welder does not stop to change electrodes, so metal goes down much faster than with stick welding. That is why MIG is the standard process for structural fabrication, machine frames, tanks and general heavy engineering. For this kind of production work the machine has to hold a steady arc at high current, run on an industrial three-phase supply and keep going through long seams without tripping.

The Paragweld MIG Series is made in India and has two industrial models, the MIG 400 I and the larger MIG 600 I. Both are designed for industrial use and weld mild steel, stainless steel and aluminium. The MIG 400 I suits general fabrication and maintenance shops, while the MIG 600 I is the higher-output choice for heavier sections. For full specifications of either model, please contact our team.
frequently asked questions (FAQ)

The MIG 400 I and MIG 600 I are manufactured in India by Paragweld, which is based in Ahmedabad. Buying a machine made in the country means you deal directly with the manufacturer for technical questions, spare parts and servicing, rather than going through an importer. Contact our team for details of support available in your area.
Decide by the thickest material you weld and the current you run most of the time. The MIG 400 I is enough for most general fabrication and repair work on light and medium sections. The MIG 600 I gives more output for thick plate, larger wire and long high-current runs. A machine far bigger than you need costs more to buy and to power, so share your job details and we will help you choose.
Both machines weld mild steel, stainless steel and aluminium, but each metal needs its own wire and gas. Mild steel is usually welded with an ER70S-6 wire under CO2 or an argon-CO2 mix. Stainless steel needs a matching stainless wire and an argon-rich gas. Aluminium needs pure argon and a soft aluminium wire, which feeds best with U-groove drive rolls and a short, straight torch cable.
For mild steel, 100% CO2 is cheaper and gives deep penetration, but it produces more spatter and a rougher bead. An argon-CO2 mix gives a smoother arc, less spatter and a neater finish, and it allows spray transfer at higher currents for faster welding on thicker plate. Stainless steel and aluminium need argon-based gases. Many shops use CO2 for structural work and a mix where appearance matters.
Most problems start at the torch and wire feed, not the power source. Clean spatter from the nozzle, replace worn contact tips, and blow out or change the liner when feeding becomes rough. Check drive roll size and tension, gas hoses for leaks, and the earth clamp and cable joints for tightness. Every few months, have a qualified person blow dust out of the machine with dry air while it is switched off and isolated.