Paragweld - Welding Machine Manufacturer in India

Parag Traders was established in GIDC, Vatva, Ahmedabad in 1980 by Mr.Parag Mashruwala to cater to the requirement of welding electrodes, equipments™ and accessories.

Welding Wire

Welding Wire Manufacturer

Welding wire is the filler metal in MIG/MAG and flux-cored arc welding, and the right grade matters as much as the machine settings. Solid wires such as AWS ER70S-6 carry extra manganese and silicon as deoxidisers, which helps them cope with light mill scale and give clean welds with very little slag under CO2 or argon-CO2 gas. Flux-cored wires such as AWS E71T-1 have flux inside a tubular sheath. The slag it forms supports the weld pool, which makes vertical and overhead welding easier on structural steel.

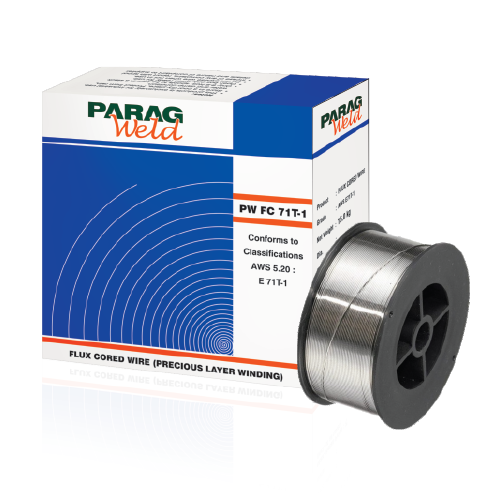
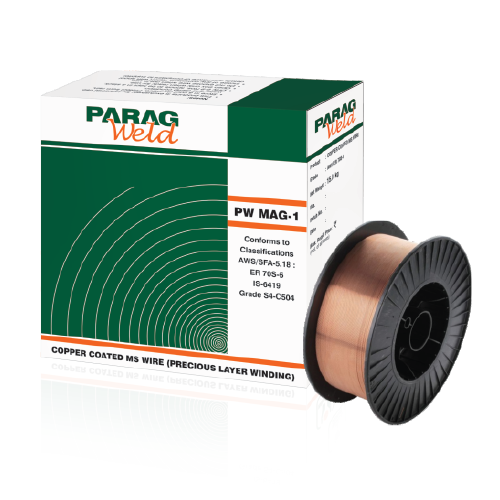
Paragweld offers one wire of each type. PW MAG-1 is a copper-coated mild steel solid wire to AWS ER70S-6, suitable for 100% CO2 or argon-CO2 mixed gas, in 0.8, 1.2 and 1.6 mm. PW FC 71T-1 is a titanium-based flux-cored wire to AWS E71T-1 for all-position welding of mild steel and 490 MPa grade high-tensile steel, in 1.2 and 1.6 mm. Both are supplied on DD 270 mm spools of 15 kg net weight.
frequently asked questions (FAQ)

Choose PW MAG-1 for general mild steel fabrication, especially flat and horizontal welds where you want a clean bead with little slag to remove. Choose PW FC 71T-1 when much of the welding is vertical or overhead, or when you are joining 490 MPa grade high-tensile steel on work such as ships, pressure vessels, mechanical equipment or steel bridges. If you are unsure, our team can advise.
Thinner wire suits thin material and lower current, while thicker wire deposits more metal on heavy plate. As a guide, 0.8 mm is used for sheet, 1.2 mm for most general fabrication and 1.6 mm for thick sections at high current. The diameter must match your machine, contact tip and drive rolls. For example, the Paragweld MIG 250F takes 0.8–1.0 mm wire, while the MIG 500 Pro takes up to 1.6 mm.
PW MAG-1 is suitable for both 100% CO2 and argon-CO2 mixed gas. CO2 is cheaper and gives good penetration, but with more spatter and a rougher bead. An argon-CO2 mix gives a smoother arc, less spatter and a neater weld face, which saves grinding on visible welds. Many fabricators use CO2 for structural work and a mix where finish matters.
ER means the wire can be used as an electrode or as a filler rod. The 70 means the weld metal has a minimum tensile strength of 70,000 psi, roughly 490 MPa. S stands for solid wire. The 6 identifies the chemical composition, which has higher manganese and silicon than most other ER70S grades. These deoxidisers help the weld tolerate light rust and mill scale on the plate.
Keep spools in their original packing in a dry, covered place until they are needed, away from floors and outside walls where condensation forms. Moisture rusts the copper coating on solid wire, causing rough feeding and porosity. Flux-cored wire can pick up moisture in the flux, which adds hydrogen to the weld. If a machine will stand idle for a long time, remove the spool and bag it.