The Five Processes at a Glance
MMA (stick) welding
A flux-coated electrode carries the current and shields the molten metal. The equipment is simple and portable, and it tolerates dirty or painted steel and outdoor conditions. It is slower than wire welding because the welder stops to change electrodes and chip slag after every run.
MIG/MAG welding
A continuously fed wire and a shielding gas produce fast, clean welds on mild steel and, with suitable wire and gas, on stainless steel and aluminium. For indoor production work it is usually the quickest route from fit-up to finished part.
TIG welding
A non-consumable tungsten electrode and a separate filler rod give the most control and the neatest bead, especially on thin sheet, stainless steel and, with an AC machine, aluminium. It is also the slowest process and the most dependent on welder skill.
Air plasma cutting
Not a joining process, but part of nearly every fabrication job. A constricted plasma arc cuts any conductive metal quickly, with a narrow kerf and little heat distortion, using only electricity and compressed air.
Submerged arc welding (SAW)
A mechanised process in which the arc burns under a blanket of granular flux. It deposits metal very quickly with deep, even penetration, making it ideal for long seams on thick plate, but it works only in the flat or horizontal position and needs a fixed setup.
Paragweld Machines for Each Process
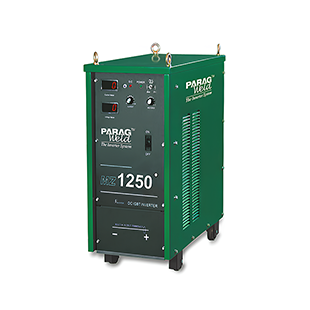
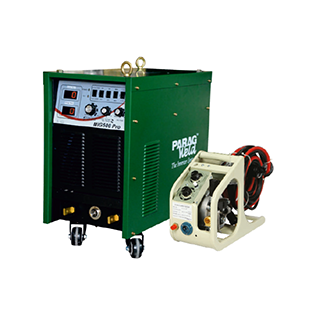
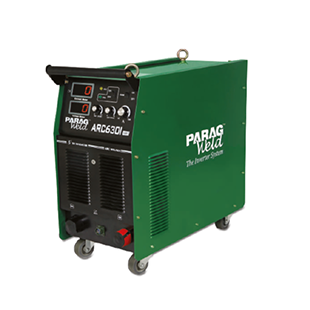
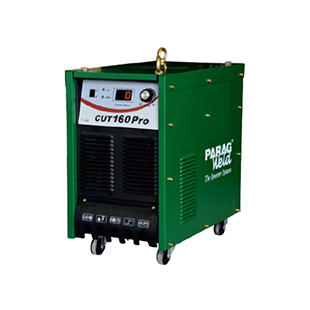
Every process in this comparison is covered by a Paragweld machine family. Open a card for specifications and model options:
Side-by-Side Comparison
| Process | Best suited materials | Speed | Portability | Typical local use |
|---|
| MMA (stick) | Mild and low-alloy steel, roughly 3 mm upwards | Moderate | High | Sugar mill repairs, site work, gates and sheds |
| MIG/MAG | Mild steel sheet to thick plate; stainless and aluminium with suitable wire | High | Medium | Fitness equipment frames, transformer tanks, machine bases |
| TIG | Thin sheet, stainless steel, aluminium, tool steels | Low | Medium | Hand-tool and die repair, stainless fittings, fine joints |
| Air plasma cutting | Any conductive metal, sheet to plate depending on model | Very high (cutting) | Medium to high | Profiles for enclosures, brackets and panels |
| Submerged arc (SAW) | Thick carbon steel plate, long straight or circular seams | Very high | Low (fixed) | Heavy tanks, cylindrical shells, thick structural seams |
Matching Each Process to Meerut's Main Trades
Sports goods and fitness equipment
Frames for gym machines, goalposts, racks and training rigs are mostly mild steel tube and sheet. MIG gives the speed and a tidy bead that needs little grinding before powder coating. A mid-range unit from the Paragweld MIG welder series handles common tube wall thicknesses comfortably; TIG is worth adding for visible stainless or aluminium parts.
Scissors and hand tools
Hardened carbon and tool steels are sensitive to heat and prone to cracking. TIG provides the low, controlled heat input needed for repairs to dies, fixtures and tooling, and a Paragweld TIG welder with fine current adjustment suits this better than MIG. Preheating and slow cooling still matter more than the machine itself.
Transformer and electrical fabrication
Transformer tanks, radiators and panel enclosures must be leak-tight and dimensionally accurate. MIG handles the tank seams, plasma cuts openings and cable entries, and TIG takes care of thin or delicate joints. Leak testing after welding remains essential whichever process is used.
Sugar mill maintenance
Mills in the region run hard through the crushing season and are repaired when it ends. Rebuilding thick, worn and often contaminated steel suits MMA welding with heavy-duty inverters from the ARC welder series, while contractors fabricating new heavy shells or structures gain most from SAW.
A Sensible Starting Combination
Most Meerut workshops do not need all five processes. A practical start is one MIG machine for production, one MMA inverter for site and repair jobs, and an air plasma cutter from the LGK series. Add TIG when stainless, aluminium or tool steel work becomes regular, and consider SAW only when heavy long seams make up a real share of your orders.
Not Sure Which Process Fits? Ask Paragweld
Send Paragweld a drawing or photo of the job along with the material and thickness, and the team will suggest a process, machine and consumable. Equipment is dispatched to Meerut from the Ahmedabad factory, and full specifications are on the products page.
Need help choosing between MIG, TIG, ARC, plasma or SAW for a job in Meerut? Call us at +91 9824099621 or email us at paragltd@yahoo.co.in for straightforward advice.