Start With the Job, Not the Machine
Buyers often ask for "a good 400-amp machine" before deciding how they will weld. That is the wrong order. The process decides your consumables, the skill your operators need, whether you need a gas supply and how fast you can work. Once the process is fixed, plate thickness and daily running hours tell you the amperage and duty cycle you need.
Three questions narrow the choice quickly:
- What material and thickness? Mild steel plate, stainless steel, aluminium, or a mix.
- Where is the weld made? On a shop floor, at height on a structure, or on an open site with wind and dust.
- How long are the seams? Short joints that are tacked and filled, or long straight and circular seams repeated all day.
MIG vs ARC vs TIG vs Plasma vs SAW at a Glance
The table compares each process under the conditions most common in local fabrication shops.
| Process |
Best suited to |
Speed |
Operator skill |
Typical local use |
| MIG / MAG |
Mild steel sheet and plate on the shop floor |
High |
Moderate |
Panels, enclosures, frames and brackets in Govindpura and Mandideep units |
| ARC (MMA) |
Structural steel, site work, repairs |
Moderate |
Moderate to high |
Steel structures, erection work and plant maintenance |
| TIG |
Stainless steel, thin sections, root passes |
Low |
High |
Stainless tanks, piping and precision parts for electrical equipment |
| Plasma cutting |
Cutting mild steel, stainless steel and aluminium |
High (cutting) |
Low to moderate |
Profile cutting and edge preparation before welding |
| Submerged arc (SAW) |
Thick plate, long straight or circular seams |
Very high |
Moderate (mechanised) |
Heavy shells, beams and structures for power equipment |
How Each Process Fits Bhopal's Industrial Work
MIG for production fabrication
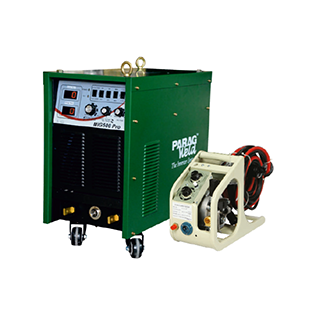
Shops in Govindpura and Mandideep make control panel frames, switchgear enclosures, trolleys and general machine parts. For this work, MIG is usually the fastest way to get consistent welds. The wire feeds continuously, so welders never stop to change electrodes, and there is little cleaning afterwards when wire and gas are matched correctly. The Paragweld MIG 500 Pro suits plate work across several shifts. Lighter models in the MIG welder series fit smaller jobbing shops.
ARC (MMA) for structures and site work
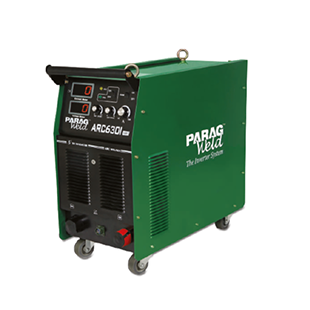
Stick welding is still the most forgiving process outdoors, at height, or on rusty and painted steel during repairs. Erection contractors and maintenance teams across the city rely on it because the machine is simple, needs no shielding gas and works with long cables. A heavy-duty inverter such as the Paragweld ARC 630i runs thick electrodes and handles gouging. Pair it with our welding electrodes.
TIG for stainless and precision joints
Suppliers to the electrical equipment sector often weld stainless steel, thin sections and parts where both appearance and control matter. TIG is slower, but it lays a clean bead with no spatter and very precise heat control. For aluminium, choose an AC/DC model from the pulse TIG AC/DC series. Pulse mode helps on thin sheet.
Plasma cutting before you weld
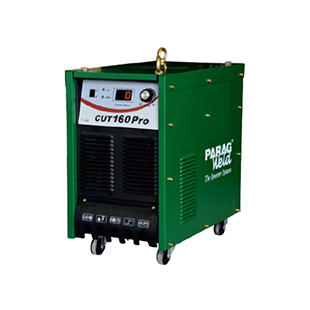
Plasma is not a welding process, but it limits how good your welds can be. An LGK or CUT series air plasma cutter makes clean, square edges quickly, which gives better fit-up and less grinding. Shops that cut many identical parts can move up to a CNC plasma system.
Submerged arc for heavy, repetitive seams
Large fabricators supplying the power-equipment sector weld long seams on thick plate: shells, beams, base frames and ducting. Submerged arc welding gives deep penetration and high deposition, with almost no spatter and no visible arc. Mount a SAW machine on a column and boom or a welding carriage, and add a rotator for circular seams. Hours of manual welding then become one mechanised operation.
Paragweld Machines for Each Process
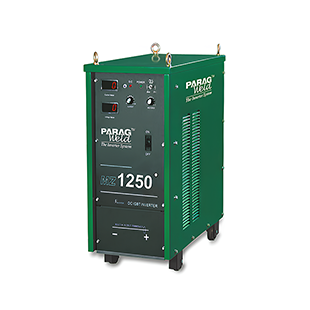
Each process in the table has its own Paragweld product line. Open a category to see models and specifications:
Process Mistakes Worth Avoiding
- Using MIG outdoors in the wind: the wind blows the shielding gas away and the weld fills with pores. Switch to ARC welding or put up screens.
- Welding thick plate in one heavy pass: several passes give better fusion and less distortion. On long seams, SAW is better still.
- Buying TIG for mild steel production: TIG welds look excellent but are slow. For high-volume mild steel work, MIG is usually the better investment.
- Choosing too low a duty cycle: when a machine trips on thermal overload in the middle of a shift, the lost time costs more than the price difference to a heavier model.
Getting Process Advice for Your Bhopal Unit
Paragweld has made welding machines in Ahmedabad since 1980 and supplies fabricators across India, including Bhopal. Send us the material, thickness and a photo or drawing of the job. Our team will suggest the right process and machine, along with matching wire, electrodes and accessories. After purchase, you can reach our service team by phone and WhatsApp.
To discuss a machine for your Bhopal workshop, call +91 9824099621 or email paragltd@yahoo.co.in. You can also send an enquiry through our contact page.