Common Welding Problems in Glass Plants and How to Fix Them
Problem 1: Cracked Welds on Furnace Structures
Why it happens: furnace binding steel, buckstays and burner brackets heat up and cool down again and again. Rigid joints, moisture in the electrodes and welding thick sections cold all encourage cracks.
The fix: use low-hydrogen electrodes stored dry, preheat heavy sections, and weld in a balanced sequence so the joint is not locked in. Where parts run hot all the time, choose heat-resistant stainless electrodes rather than ordinary mild steel rods. A stable inverter such as the Paragweld ARC 400G keeps the arc smooth at the settings these electrodes need.
Problem 2: Distortion in Lehr Frames and Conveyors
Why it happens: annealing lehrs and conveyor structures are long, fairly light frames. Long continuous welds put in more heat than the frame can take, and it bows.
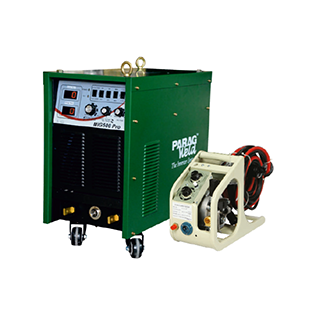
The fix: tack thoroughly, use skip or stitch welding, and alternate sides. MIG welding with carefully set parameters puts in less heat per metre than slow stick runs, and a machine like the Paragweld MIG 400 Pro gives fine control. For thin stainless supports and belt guides, pulse TIG keeps heat input to a minimum.
Problem 3: Porosity from Scaled or Dirty Steel
Why it happens: steel near furnaces picks up oxide scale, oil and soot, and electrodes left in a humid shed absorb moisture. Strong draughts from combustion fans can also blow away MIG shielding gas.
The fix: grind back to bright metal, keep electrodes in a dry cabinet, and screen the MIG area from fans. Where a draught can't be avoided, switch to stick welding, which needs no gas.
Problem 4: Heavy Spatter and Slow Cleanup
Why it happens: wire speed and voltage out of balance, a worn contact tip, poor-quality wire or the wrong gas.
The fix: retune the machine for the wire size, replace consumables on time, and use consistent welding wire that feeds smoothly. Less spatter means less grinding, and less spatter stuck on conveyor parts that touch hot glass.
Problem 5: Welding Machines Overheating in a Hot Plant
Why it happens: the air around furnaces is already hot, and fine batch dust from sand and other raw materials clogs cooling paths inside the machine.
The fix: keep the machine as far from the furnace as the leads allow, clean it out with dry compressed air regularly, and stay within its duty cycle. For long TIG jobs, a water cooling unit keeps the torch working without overheating.
Problem 6: Slow, Rough Cutting During Repairs
Why it happens: gas cutting is slow on thin and medium plate and leaves edges that need grinding before welding.
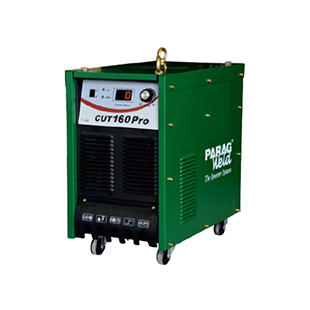
The fix: an air plasma cutter such as the Paragweld CUT 105 Pro cuts mild steel and stainless quickly with a clean edge, which shortens repair work during a shutdown.
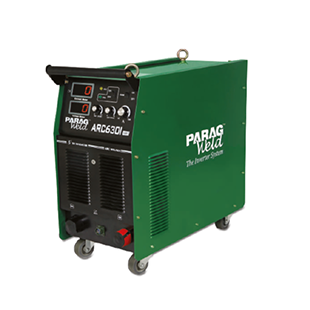
Machines and Consumables Referred to Above
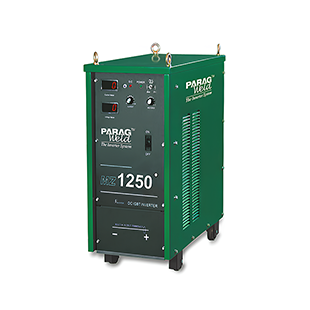
These are the Paragweld product families behind the fixes described on this page:
Planning Welding Work Around Furnace Shutdowns
In a glass plant the repair window is short and costly, so preparation decides how the job goes. Before a planned shutdown, list the repairs, cut plates and sections in advance, test every machine, and stock enough electrodes, wire and torch parts for the whole job. Assign each welder a process that suits the task: stick for structural steel close to the furnace, MIG for frames in the workshop, and TIG for stainless parts.
Problems and Solutions at a Glance
- Cracking: low-hydrogen or heat-resistant electrodes, preheat, balanced welding sequence.
- Distortion: stitch welding, MIG or pulse TIG with controlled heat input.
- Porosity: clean metal, dry electrodes, shelter from fan draughts.
- Spatter: correct settings, fresh contact tips, good wire.
- Machine overheating: distance from the furnace, dust cleaning, water-cooled torches.
- Slow cutting: air plasma instead of gas on thin and medium plate.
Speak to Paragweld About Your Firozabad Plant
Tell us which problem you are fighting, what you are welding and in what conditions, and we will suggest a machine and consumables to match. Paragweld delivers to Firozabad, and the full product range is online.
Call us at +91 9824099621 or email paragltd@yahoo.co.in for help with welding in your Firozabad glass or bangle unit.