The Five Processes and Where Each One Fits
MIG/MAG: Speed for Production Work
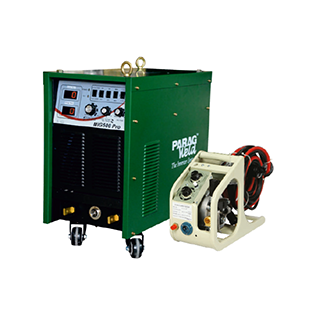
MIG welding feeds a continuous wire through the torch under shielding gas, so the welder does not stop to change electrodes. That makes it the process of choice for batch production: brackets, cross-members, cabin frames and trailer bodies of the kind made by commercial-vehicle suppliers near Dharwad. It needs a gas cylinder and a sheltered area, so it belongs in the shop. A three-phase machine such as the Paragweld MIG 400I covers most medium-section fabrication.
ARC (MMA): The Dependable All-Rounder
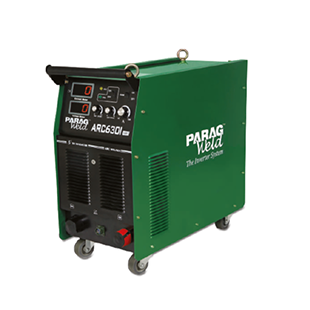
Stick welding with coated electrodes needs no gas, tolerates wind and less-than-clean surfaces, and works in any position. That is why it remains the standard for repair and maintenance, from the railway workshops in Hubballi to field repairs on ploughs, harvester frames and tractor trailers. It is slower than MIG and leaves slag to chip, but no other process is as versatile.
TIG: Control for Thin and Critical Welds
TIG gives the welder precise control of heat and filler, producing clean, spatter-free welds on stainless steel, thin sheet and root passes in pipe. It is slower and needs a skilled hand. With an AC/DC machine such as the Paragweld TIG 315P AC/DC, the same unit can weld aluminium, which is useful for equipment repair shops and units making precision parts.
Air Plasma Cutting: Fast, Clean Profiles
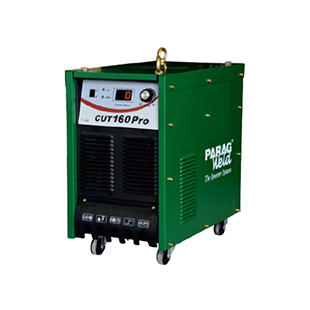
Plasma is a cutting process, not a welding one, but it decides how quickly a job reaches the welder. Agricultural implement makers cutting blades, brackets and plates find plasma far faster and cleaner than gas cutting on thin and medium plate, and it cuts stainless and aluminium as well. The CUT 105 Pro suits regular workshop cutting; CNC plasma systems take over when profiles repeat in volume.
Submerged Arc: Long Seams on Thick Plate
In submerged arc welding (SAW), the arc runs under a blanket of granular flux, giving deep penetration and very high deposition with almost no visible spatter or arc flash. It suits long straight or circular seams on thick plate: heavy frames, beams, tanks and large structures. It is almost always mechanised, mounted on a tractor carriage or a column and boom, and is not suited to positional or site repair work.
MIG vs ARC vs TIG vs Plasma vs SAW: Comparison Table
| Process |
Typical twin-city job |
Speed |
Operator skill |
Site / outdoor use |
Finish |
| MIG/MAG |
Vehicle component batches, trailer bodies |
High |
Moderate |
Limited (needs gas shielding) |
Good, light spatter |
| ARC (MMA) |
Railway workshop repair, farm machinery field repair |
Moderate |
Moderate |
Excellent |
Fair, slag to remove |
| TIG |
Stainless parts, thin sheet, pipe root passes |
Low |
High |
Limited |
Excellent |
| Air plasma cutting |
Implement blades, brackets, plate profiles |
High |
Low to moderate |
Good (portable units) |
Clean cut edge |
| Submerged arc |
Thick-plate frames, tanks, long seams |
Very high |
Low (mechanised) |
Not suitable |
Excellent, smooth bead |
Paragweld Machines for Each Process
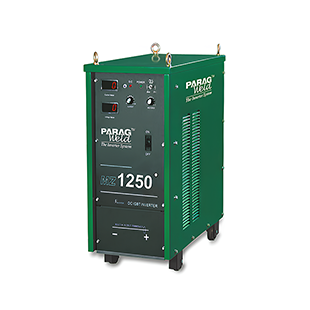
Each process in the table maps to one of these Paragweld product families:
Which Combination Suits Your Hubballi-Dharwad Workshop?
- Component supplier to a vehicle plant: MIG for production, plasma for blanks, and one ARC inverter for fixture repair.
- Railway-related repair and maintenance work: ARC inverters with low-hydrogen electrodes as the mainstay, with TIG for any stainless or thin-section repairs.
- Agricultural machinery maker: plasma cutting and MIG welding as the core pair, adding a welding rotator or carriage as volumes grow.
- Heavy engineering or structural unit: submerged arc welding for long seams, backed by MIG and ARC for fit-up and tack work.
Get Process Advice Before You Buy
If you are unsure which process your jobs need, describe the part, material and thickness to our team and we will explain the options. Paragweld supplies and delivers to Hubli-Dharwad and supports buyers by phone and WhatsApp. Browse the full product range for every process covered here.
Looking for the right welding process and machine in Hubli-Dharwad? Call us at +91 9824099621 or email paragltd@yahoo.co.in.