Five Processes Compared for Prayagraj Fabrication
Most workshops that grow beyond one or two welders end up using more than one process. The key is knowing where each one earns its keep.
ARC (MMA / Stick) Welding: The Site Workhorse
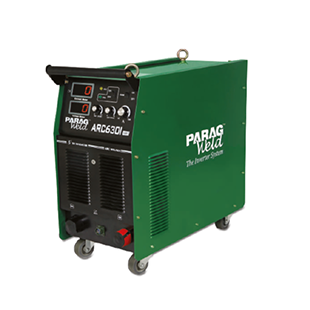
Stick welding needs no shielding gas, handles wind, and keeps working when the steel is not perfectly clean. That makes it the natural choice for bridge-side work, girder repairs, foundation steel and railway maintenance jobs done outdoors. With low-hydrogen electrodes it produces sound structural welds in every position. A high-output inverter such as the Paragweld ARC 630i can run larger electrodes and long cable leads to the work.
MIG/MAG Welding: Speed on the Shop Floor
Inside a Naini fabrication shed, MIG welding is usually the most productive process. Continuous wire feed means fewer stops, faster fillet welds and less slag to remove, which matters on repeat work like brackets, frames, platforms, cable trays and fabricated sections. Shielding gas can be disturbed by wind, so MIG belongs indoors or behind screens. The Paragweld MIG 500 Pro is built for heavy, multi-shift fabrication.
TIG Welding: Precision Where It Counts
TIG is slower, but it gives the most control. Use it for stainless steel, thin sections, pipe root passes and any joint that must be neat and leak-tight. In Prayagraj it typically fits stainless process piping, instrument supports and the finishing work that follows heavy fabrication.
Air Plasma Cutting: Clean Preparation
Good welds start with good cuts. An air plasma cutter cuts mild steel, stainless and aluminium using only compressed air and electricity, and it leaves a narrower heat-affected edge than gas cutting on thinner plate. Fabricators use it for gusset plates, cleats, stiffeners and trimming sections. The LGK air plasma cutter series covers a range of cutting capacities.
Submerged Arc Welding: For Long, Heavy Seams
When the work involves long straight seams on thick plate, such as built-up I-girders, box sections, bridge members or large tanks, submerged arc welding becomes worth the investment. The arc runs under a blanket of flux, which gives deep penetration and high deposition with almost no spatter or visible arc. It needs a tractor, carriage or column and boom to move the torch, so it suits shops with steady heavy-plate work.
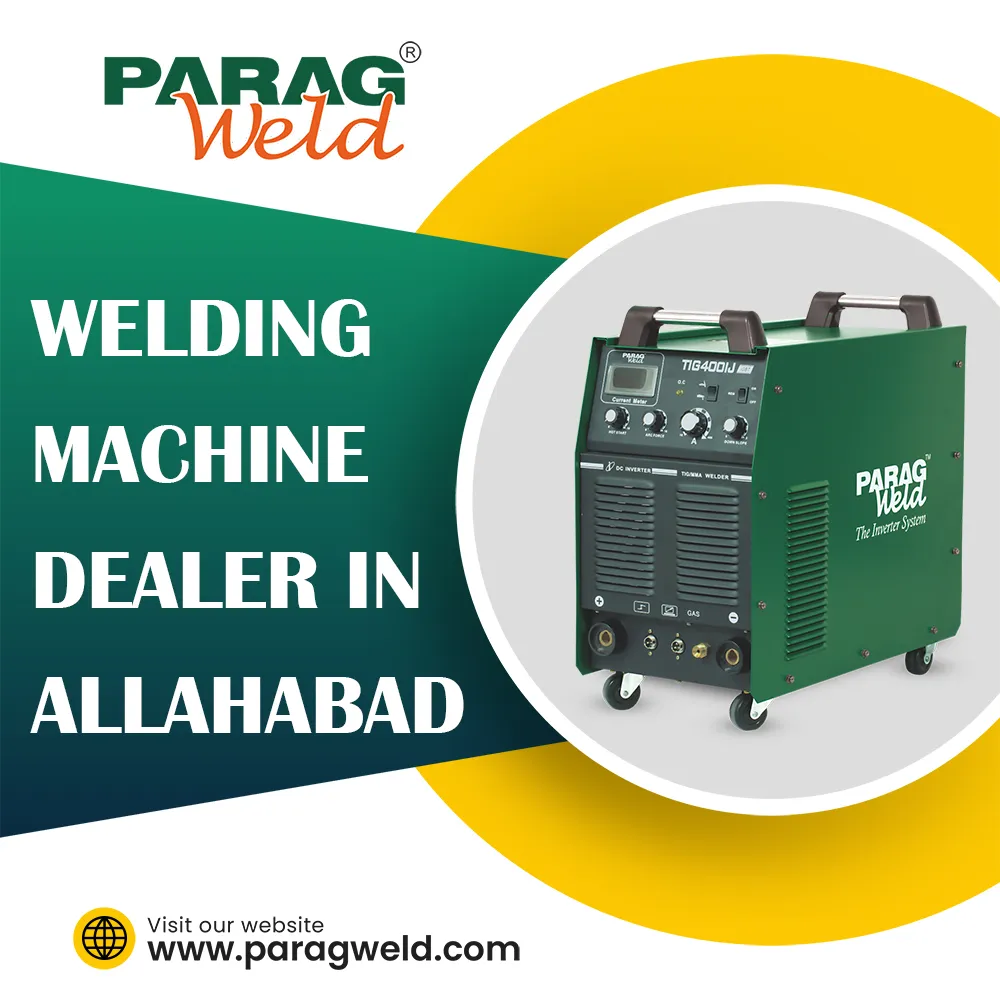
Paragweld Machines for Each Process
The machine families below correspond to the processes compared above:
Side-by-Side: Which Process for Which Prayagraj Job?
| Process |
Typical Prayagraj job |
Site or shop |
Speed |
Operator skill |
| ARC (MMA / stick) |
Bridge and girder repairs, railway maintenance, outdoor structural work |
Site and shop |
Moderate |
Moderate |
| MIG/MAG |
Repeat fabrication, frames, platforms, brackets in Naini sheds |
Shop (sheltered) |
High |
Low to moderate |
| TIG |
Stainless piping, thin sheet, pipe root passes, finishing work |
Shop |
Low |
High |
| Air plasma cutting |
Gussets, cleats, stiffeners, trimming plate and sections |
Site and shop |
High |
Low |
| Submerged arc (SAW) |
Long seams on built-up girders, box sections, tanks |
Shop |
Very high on long seams |
Moderate (setup matters most) |
Where Should a Prayagraj Workshop Start?
- Small fabricators taking site and railway maintenance jobs: a stick inverter plus an air plasma cutter covers most work.
- Naini shops doing steady shop fabrication: make MIG the main process, keep a stick machine for site visits, and add plasma for cutting.
- Firms bidding for girder or heavy-plate work: add a SAW machine with a column and boom or carriage.
- Units handling stainless or pipework: add a TIG machine for root passes and visible joints.
Supply and Support in Prayagraj
Paragweld delivers machines, welding electrodes and welding wire to Prayagraj. All its industrial machines run on three-phase 415V, so plan the supply and earthing before installation. The team helps by phone and WhatsApp with process selection, parameter settings and spare parts. If you are unsure which process a new contract needs, send us the drawing or a description of the joints, the plate thickness and whether the work is on site or in the shop, and we will suggest a combination of machines that fits the job and your budget.
Call us at +91 9824099621 or email paragltd@yahoo.co.in to work out which process and machine fit your jobs in Allahabad.